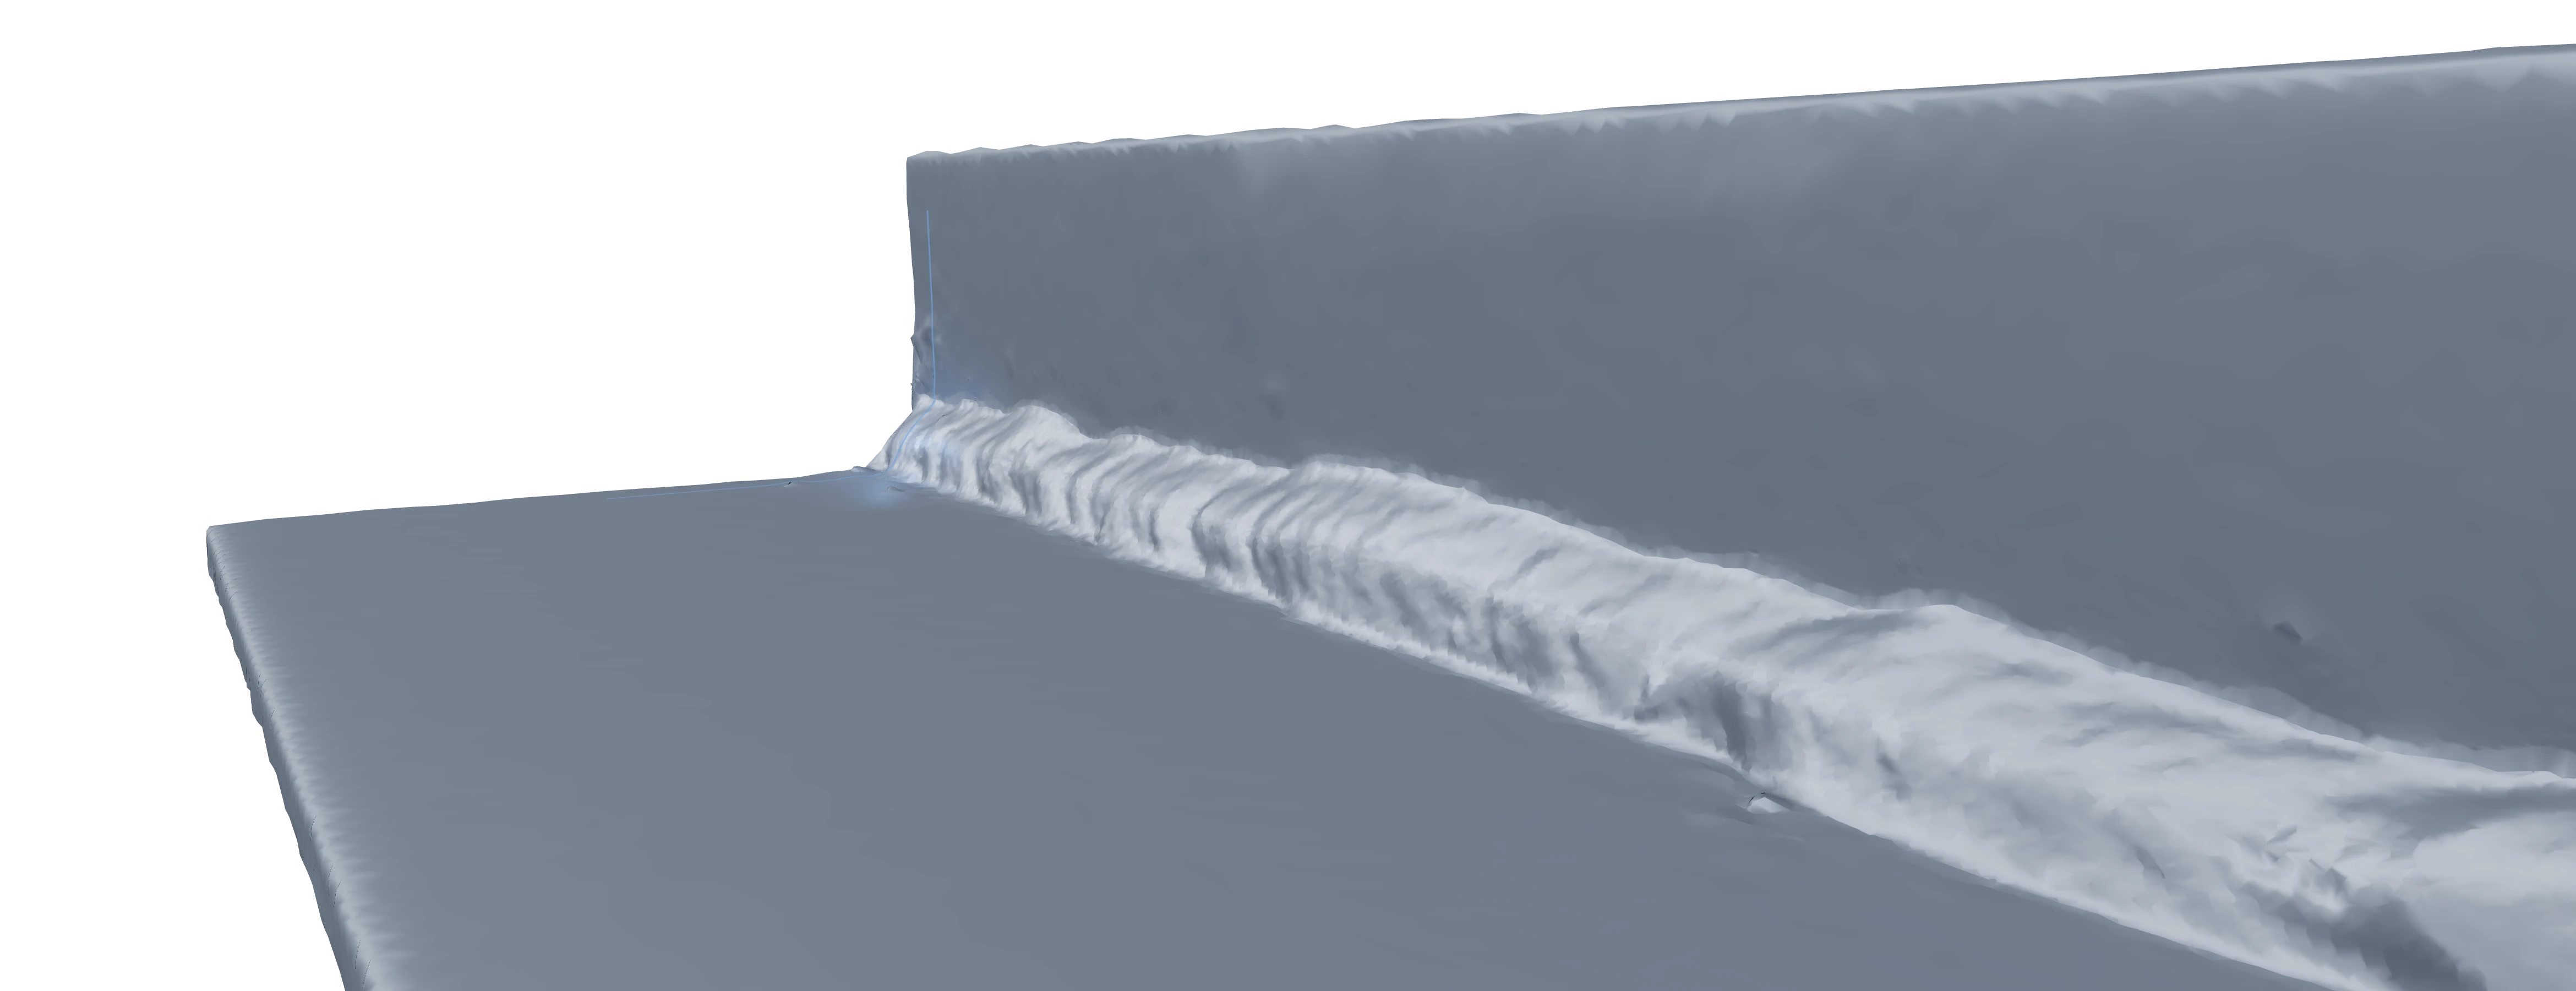
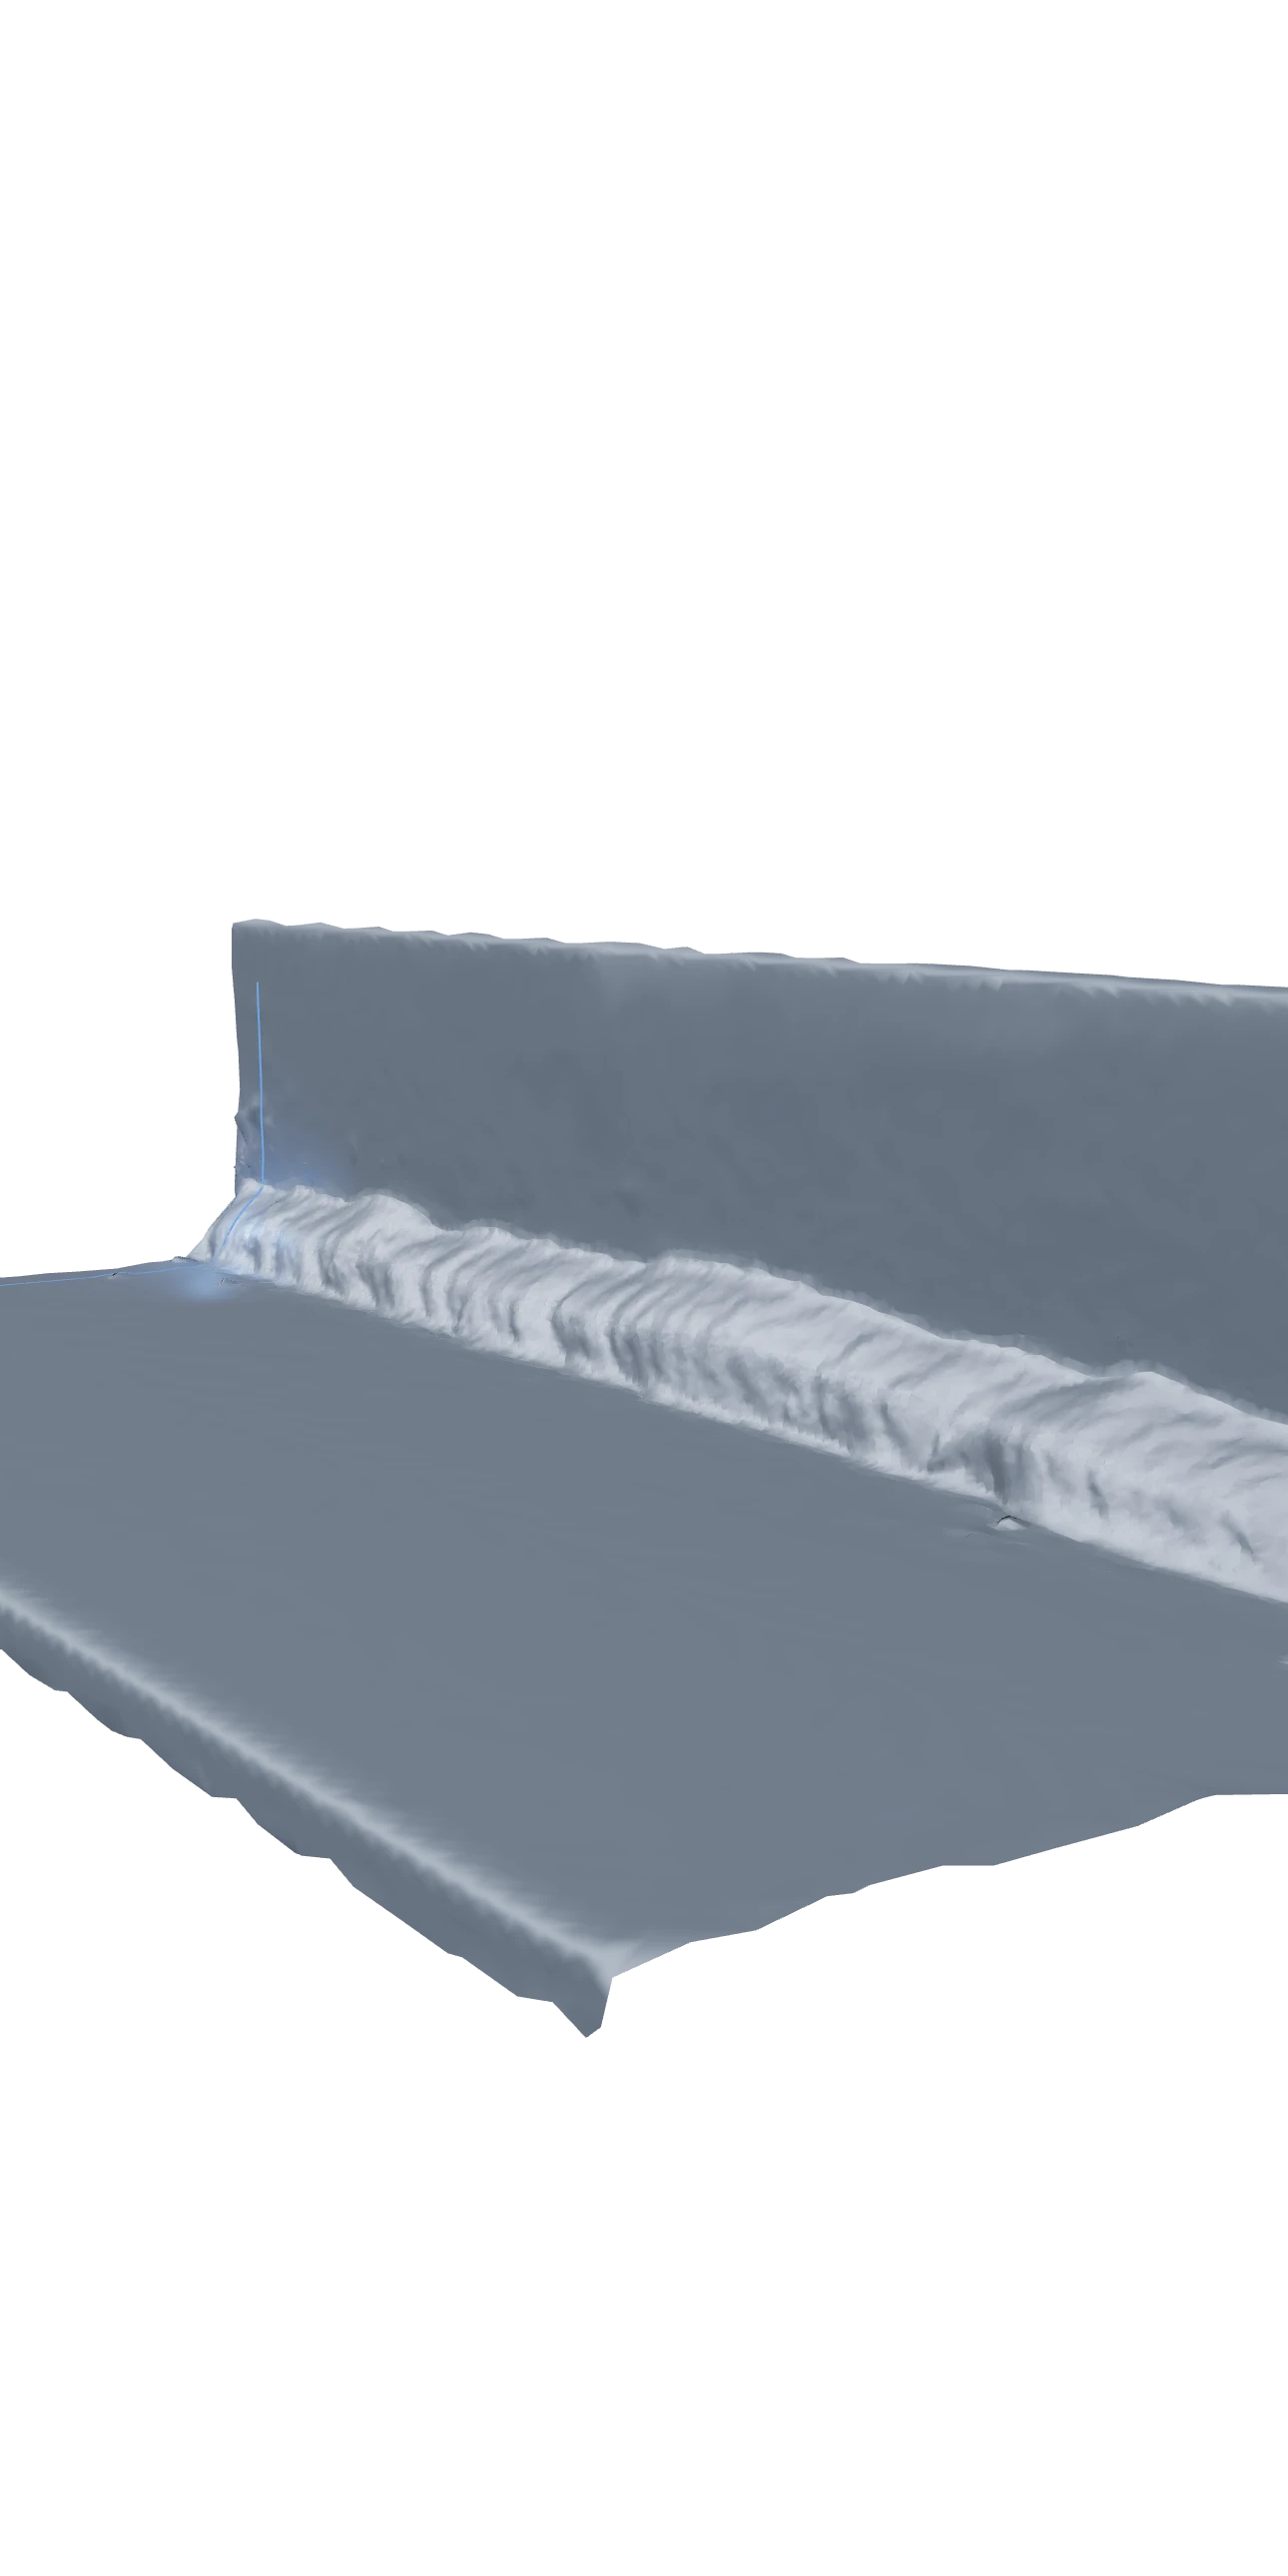
Recorded weld 104
01 / How it works
SynSpectAI Weld Inspection
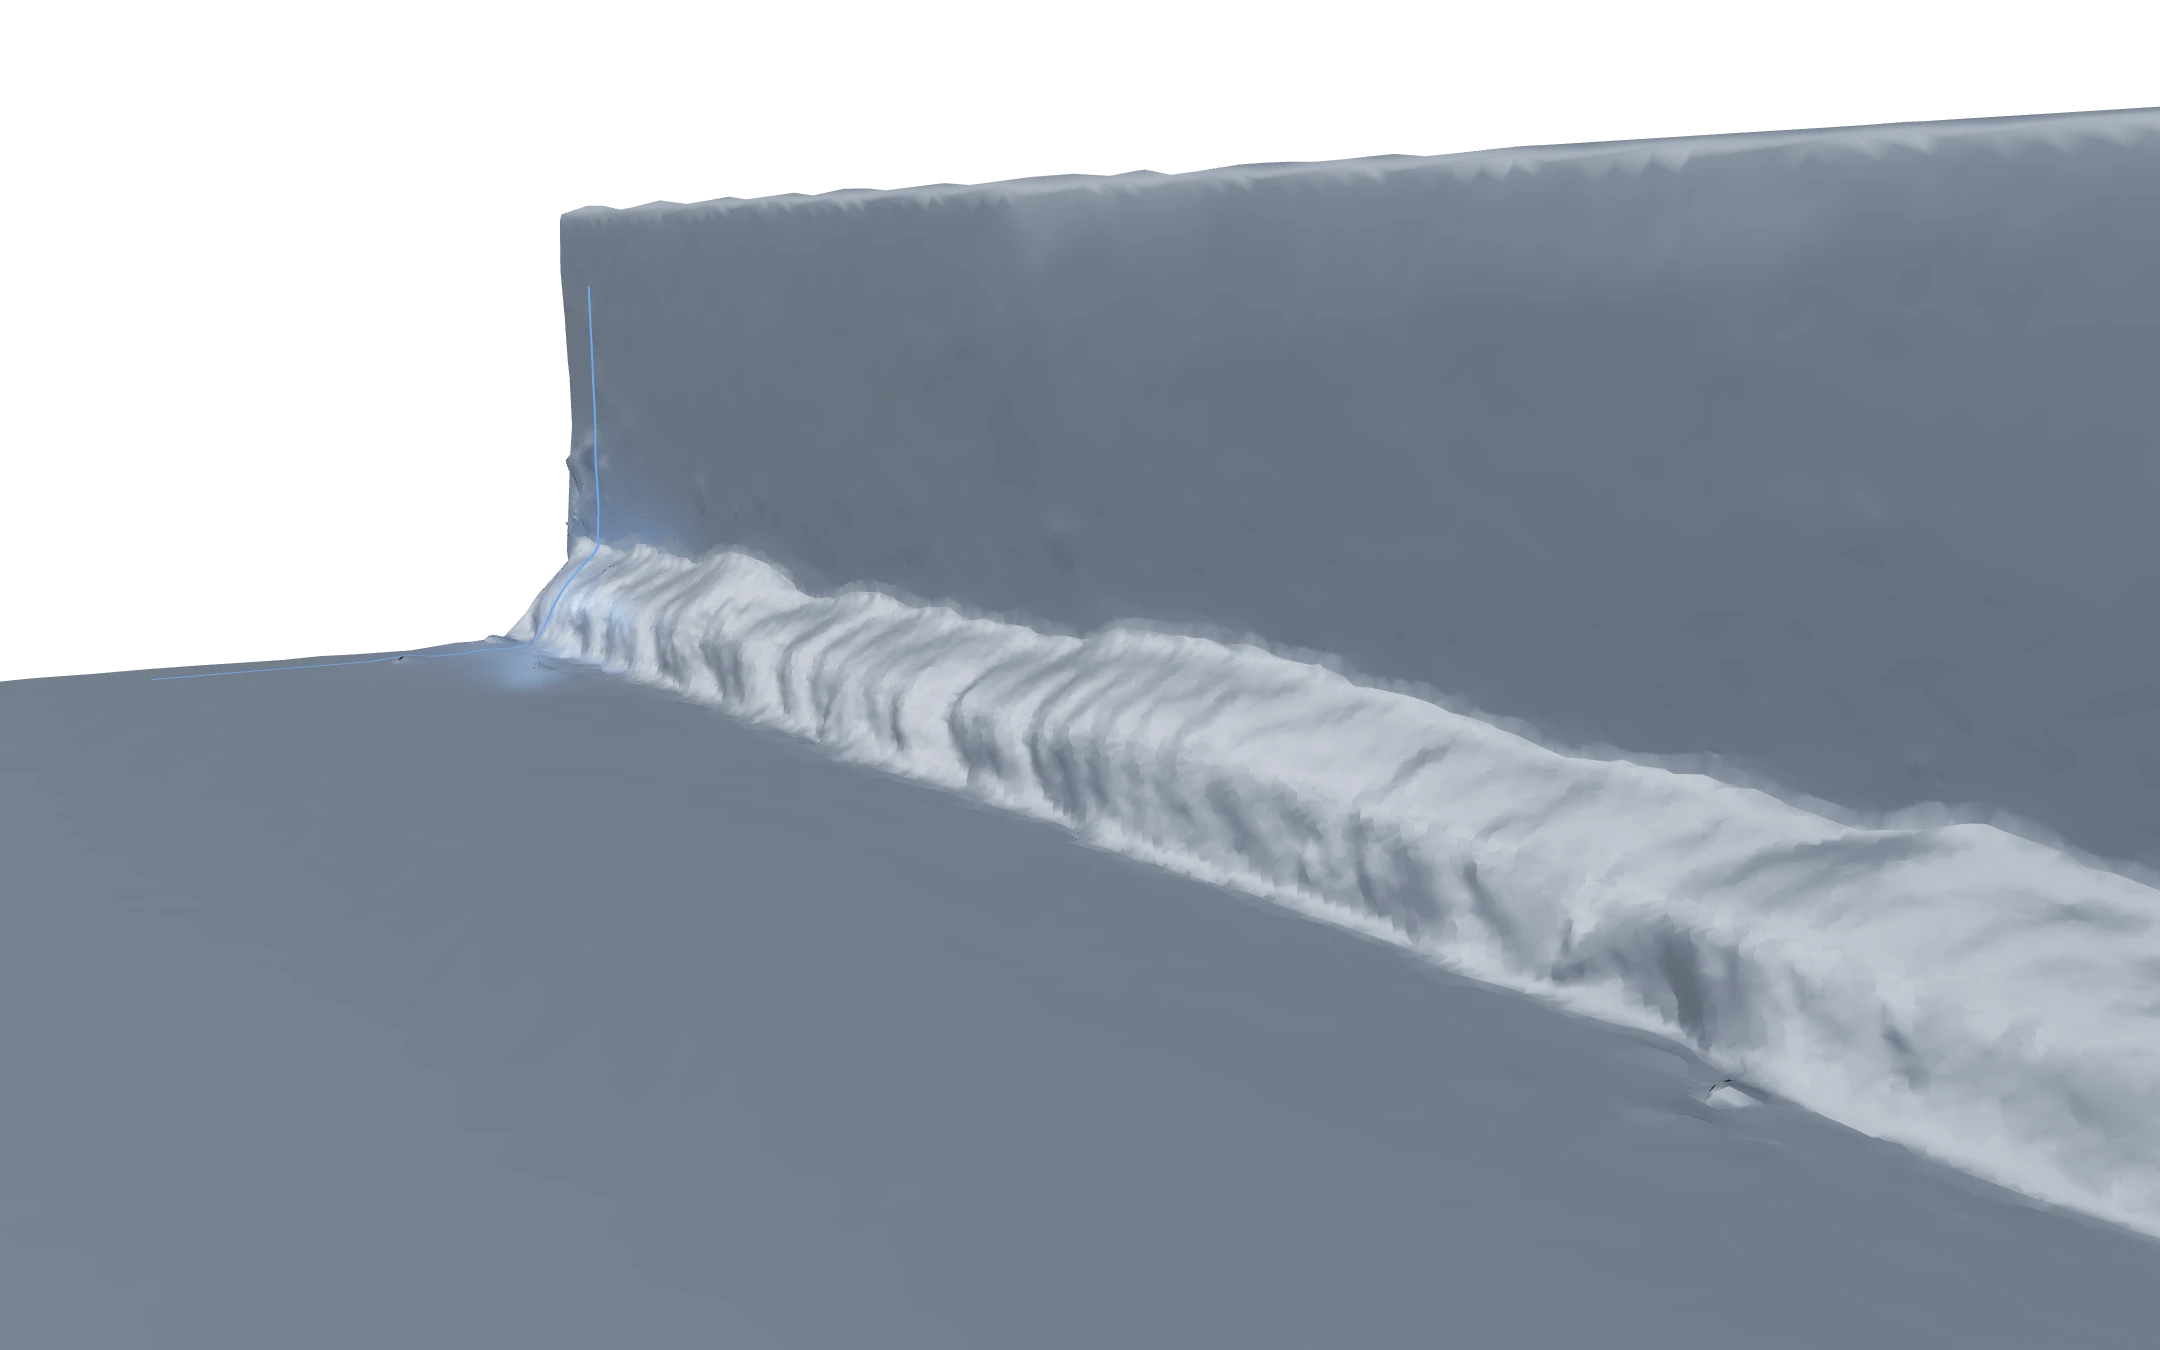
SynSpectAI Weld Inspection
Every weld, checked against the code, on the scanner you already own. Your inspector keeps final sign-off.
How it works
From scan to record in four steps.
01
Scan
Your profiler or scanner captures the weld surface.
02
Measure
SynSpect isolates the weld and takes its readings on every cross-section along its full length.
03
Judge
Each reading is checked against the code limits for that weld recipe: pass, check, or fail.
04
Record
An immutable record with per-cross-section evidence goes to your quality system.
Backed by
- Entrepreneurial Summer Incubator (ESI)
- Western University D2M Lab
- Pursuing a partnership with CWB Group
The problem
Weld inspection is still done visually and with hand gauges, by a shrinking pool of certified inspectors.
Time
37 s
for a 140-weld frame
A roughly 140-weld truck frame gets about 37 seconds of inspection at a major auto plant. That is 0.26 seconds per weld.
Missed defects
1 in 101
defects missed
About 1 in 10 defects are missed in manual inspection, according to local manufacturers.
Workforce
$110K2
per inspector, per year
Certified inspectors are retiring faster than new ones are entering the trade. One certified inspector costs about $110K a year, loaded.
- 1Reported to SFI by local manufacturers. This is not an industry-wide statistic.
- 2Loaded cost: AWS median pay plus the BLS benefits rate. Retirement trend: AWS.
What you get
Inspection you can measure, trace, and keep.
The product
A measurement, a record, and a recommendation for each weld.
SynSpect measures each weld, checks every reading against the code limits for that weld, and keeps the record.
Fig 1.1
Run an inspection
Press run to inspect a recorded weld. Each run picks another one.
- Code
- CSA W59
- Joint
- T-joint, fillet
- Weld
- 5 mm fillet
- Parent
- 8 mm plate
| Reading | Measured | Limit | Verdict |
|---|---|---|---|
| Leg length, vertical | ··· | ··· | |
| Leg length, horizontal | ··· | ··· | |
| Throat thickness | ··· | ··· | |
| Reinforcement height | ··· | ··· | |
| Convexity (face bulge) | ··· | ··· | |
| Concavity (face dip) | ··· | ··· |
WELD-104 2026-09-16 11:00
Recorded weld 104
Fig 1.2
See beyond pass / fail
Every flagged reading is pinned to where it was found. Drag to rotate, hover a marker for the reading.
See the full product
Every reading, the verdict logic, the check band, inspection records, and answers to common questions.
- Readings
- Verdicts
- Check band
- Records
- FAQ
Proprietary AI
Deployed with 10 training samples.
Most inspection AI needs thousands of hand-labelled welds before it works. SynSpect runs on proprietary AI models built in-house to need far fewer, so a new deployment takes about 10 samples from your line.
- 1From SFI development work. Sample counts vary with joint type and scanner.
- 2Agreement with ground truth in SFI testing to date.
- 3From SFI testing to date.
Start with one part on your line.
We run SynSpect against your own gauges, and you decide when it goes live.